Conveyor Technologies: low-profile conveyor systems from Milford, Ohio
Low-profile conveyor systems
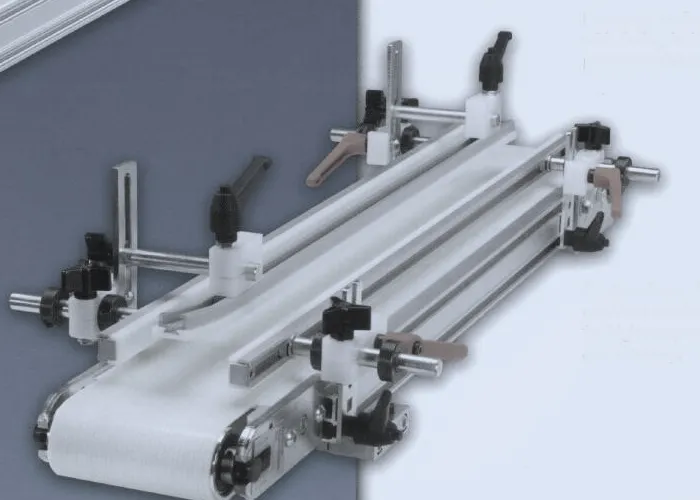
Low-profile conveyors, built to be maintained.
Designed around your part and your machine, and engineered so a belt change is a short planned job.
See the range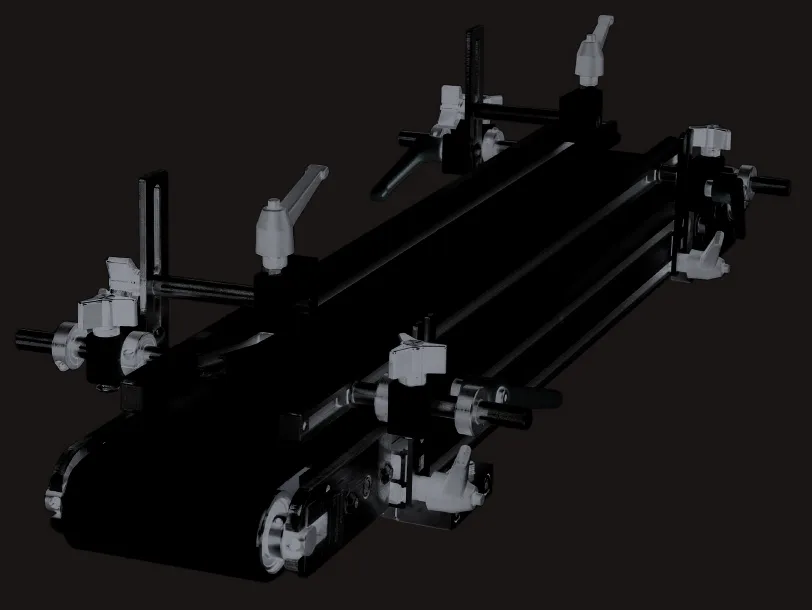
Why Conveyor Technologies
Designed around your part. Built around your maintenance.
Every conveyor we make starts with the job it has to do, and the people who will keep it running.
How we design01 · Built to be maintained
Maintenance is a short planned job, not a shutdown.
- Sealed bearings
- No routine relube
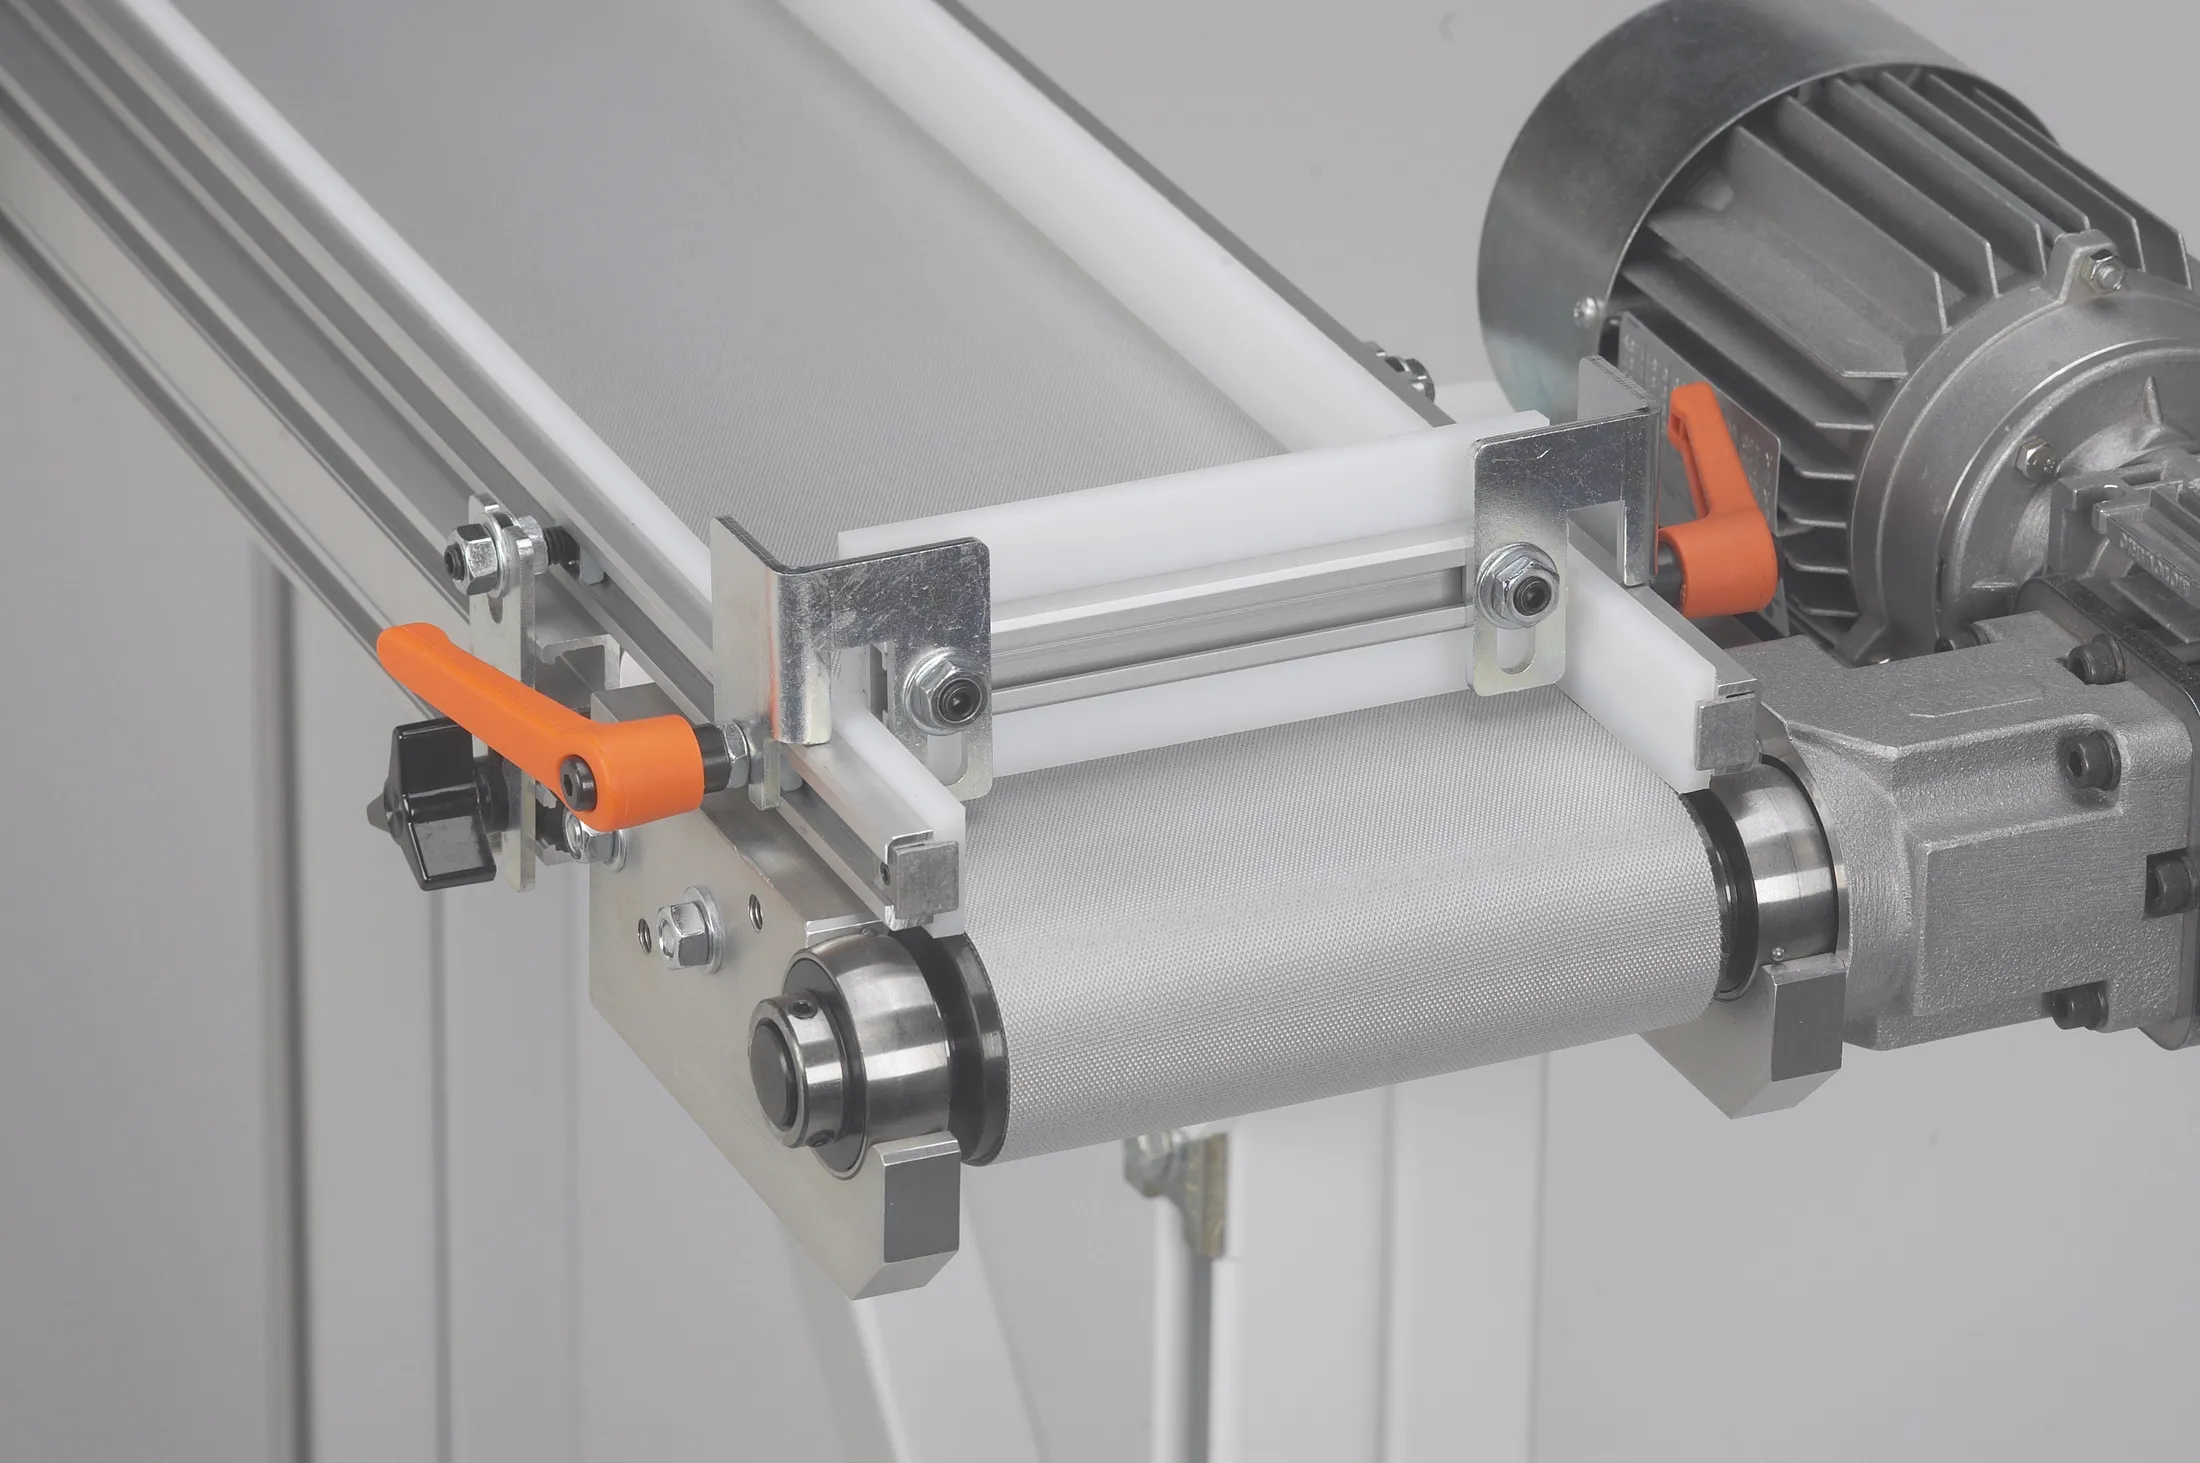
- Calibration gauges
- Each side
- Belt change
- Without tools
02 · One modular system
14conveyors on one modular concept, with components that interchange across the range.
03 · Designed for your machine
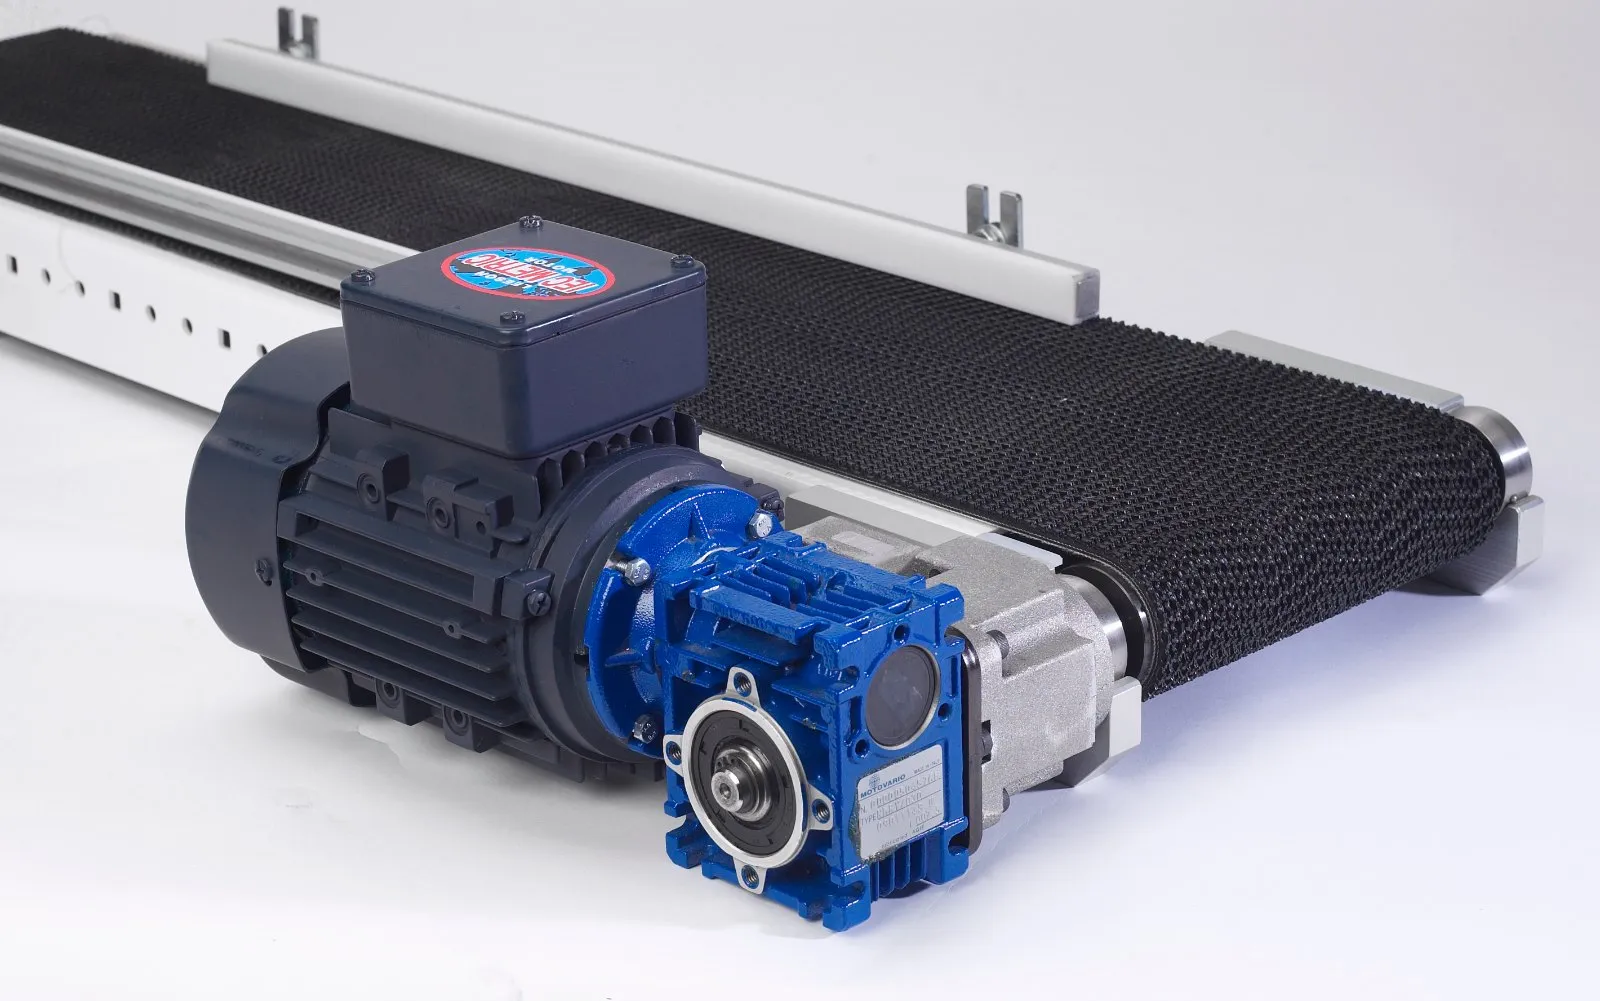
The drive goes wherever your machine leaves room.
- End
- Center
- Underneath
- Right angle
- Shaft mounted
What we make
One modular system, from belt to stand.
Conveyors, drives, guides and stands designed to work together, so every arrangement we build for you uses parts you can get again.
All products14 products
Conveyors
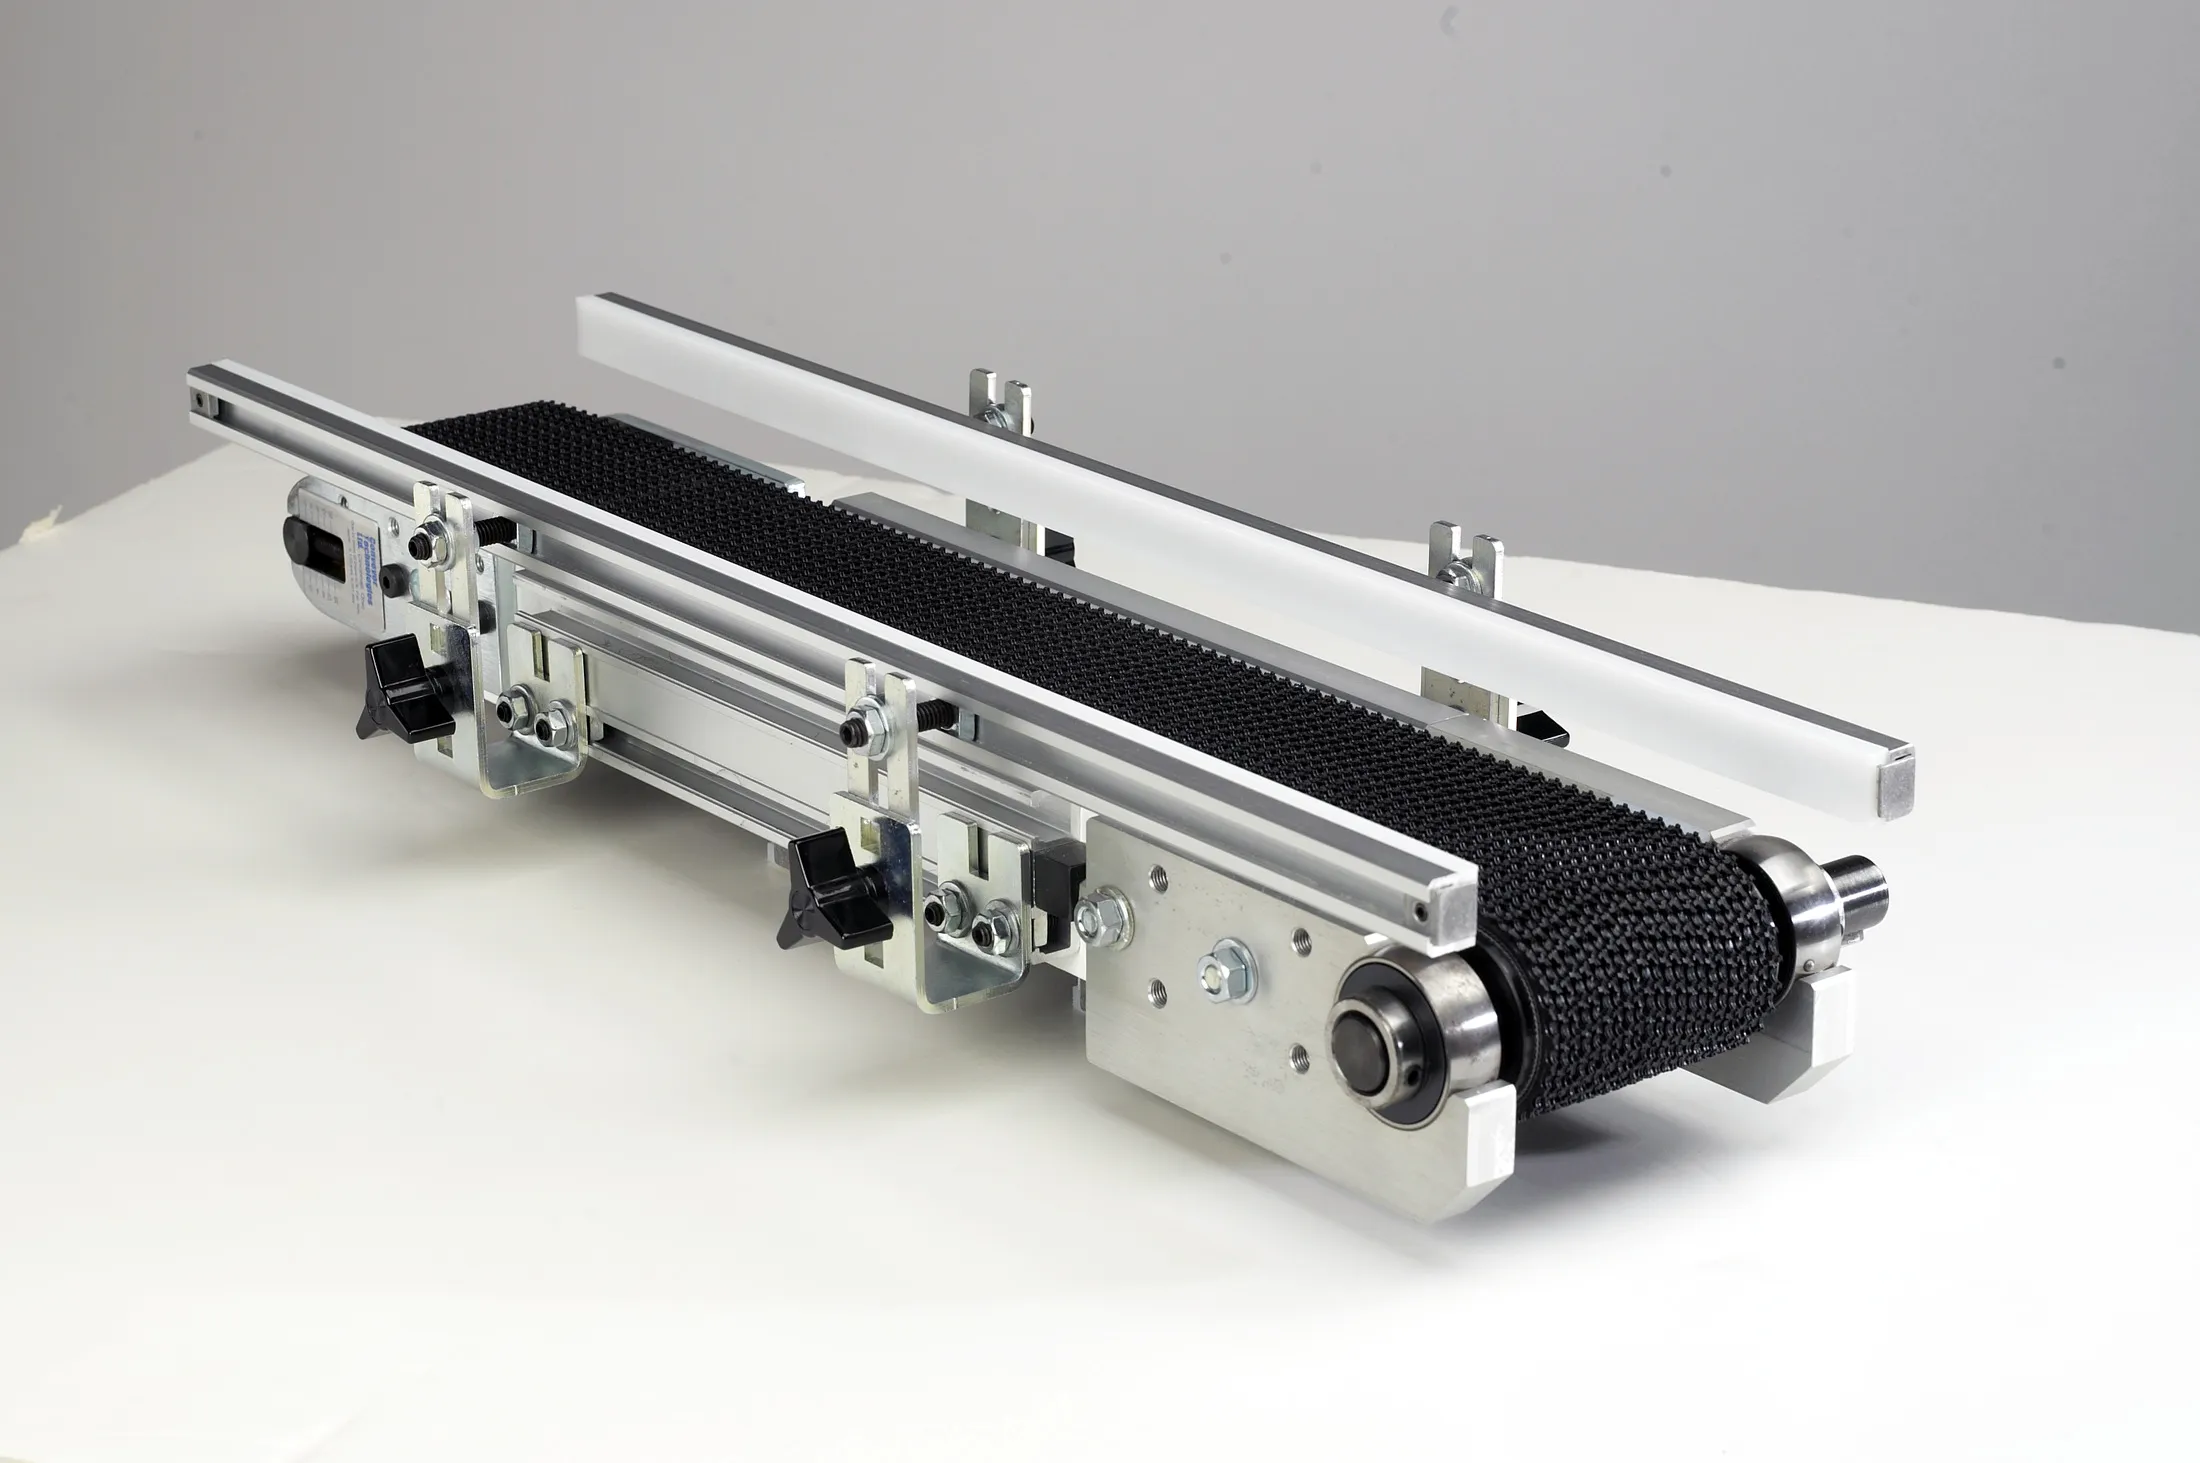
Flat belt, timing belt, vacuum, mesh, cleated and more.
Explore
7 arrangements
Drive systems
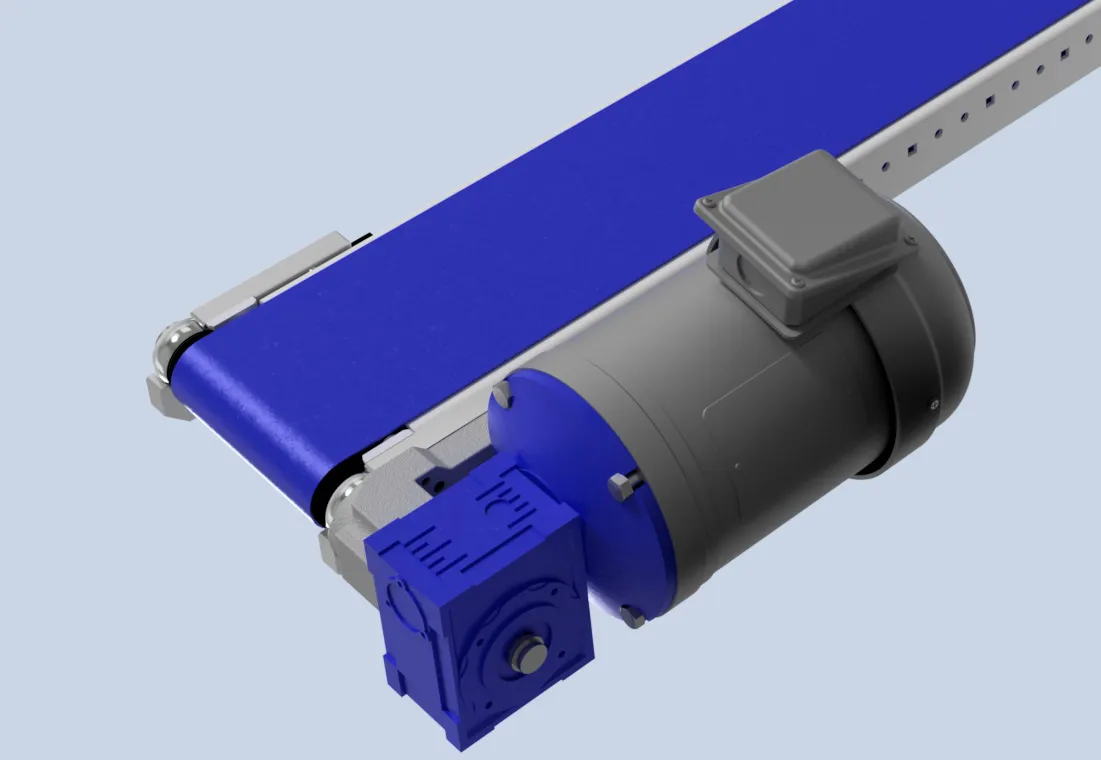
End, bottom, right-angle and shaft-mounted gearmotors.
Explore
3 types
Side guides
Fixed, two-axis adjustable and hold-down.
Explore
2 types
Conveyor stands
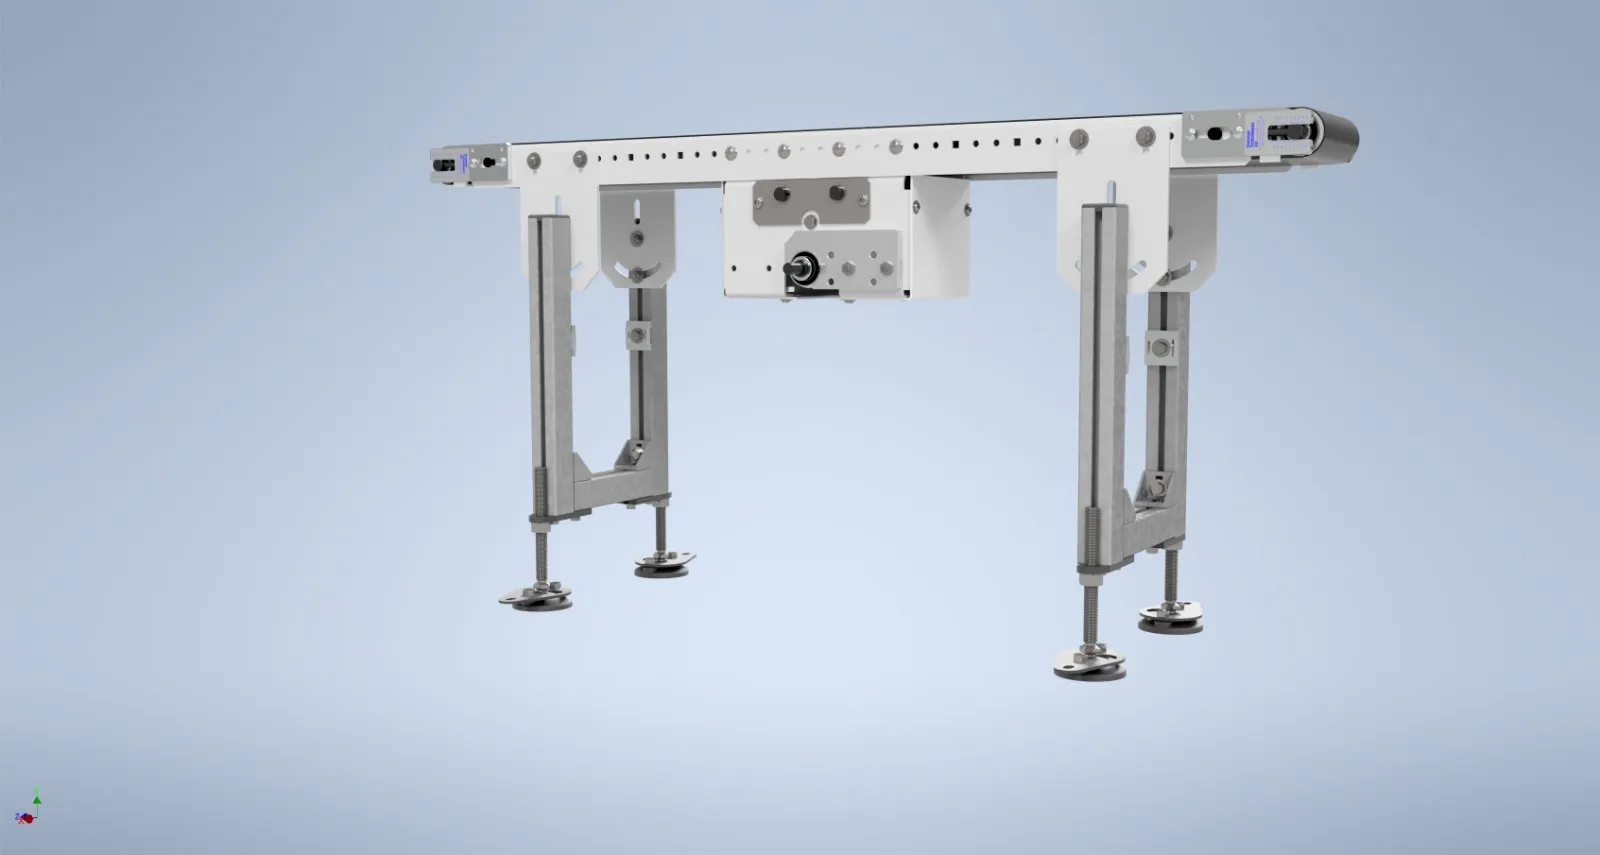
Aluminum and steel, with height adjustment.
Explore
One system, every job
Fourteen conveyors. Seven drives. One modular system.
Components interchange between conveyor types and share our standard drives and accessories, so each new line is simpler to run than the last.
- conveyors, one patented system
- 14
- drive arrangements
- 7
- typical FlexLoc part positioning
- ±0.01in
- routine bearing relubrication
- 0
Featured conveyors
Engineered for the job it does.
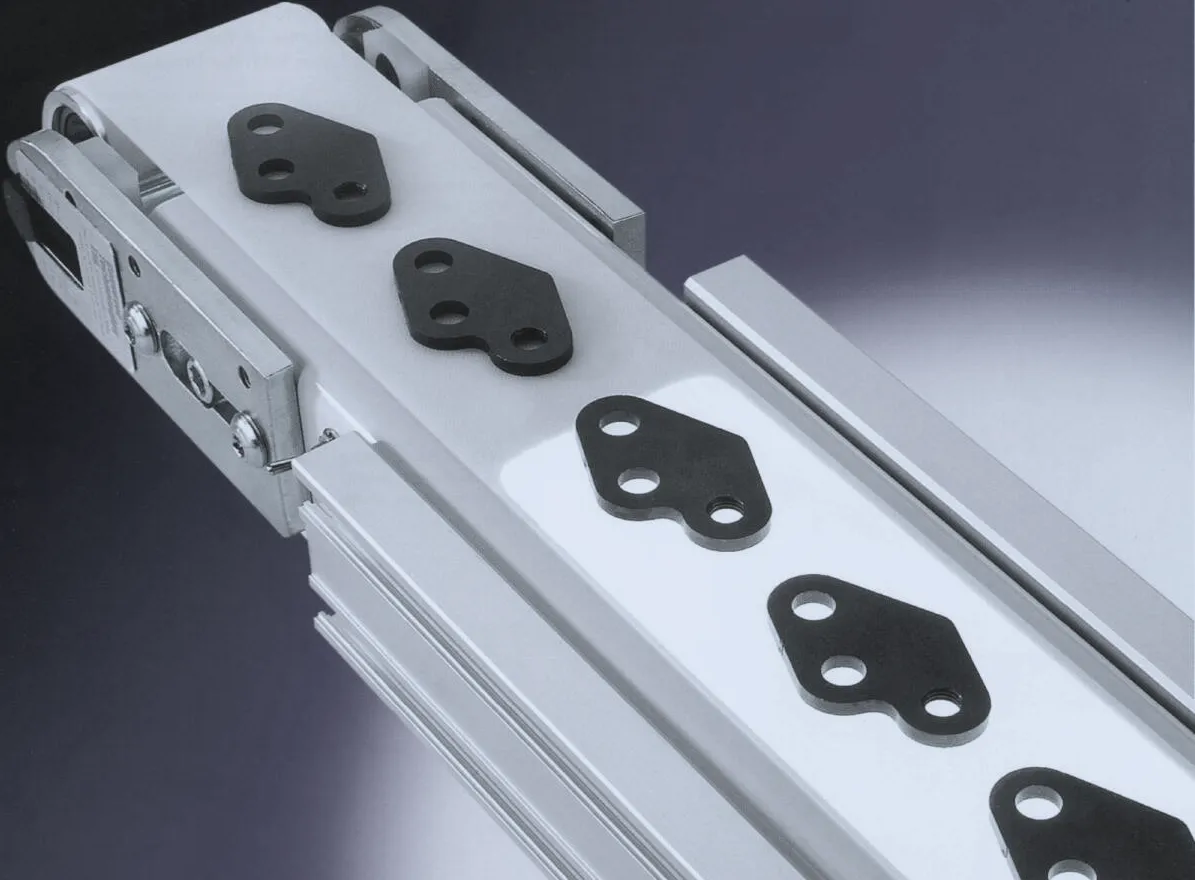
Vision inspection
The belt is the backlight.
Parts ride over an illuminated belt, so the camera sees a clean, high-contrast profile without separate lighting under the conveyor.
- Light
- White or red LEDs
- Belt change
- 2 min on our open stand
- Frame
- T-slot aluminum rails
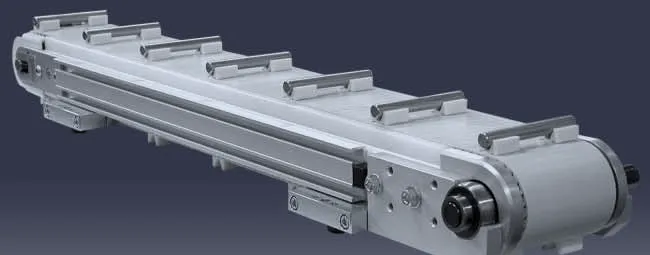
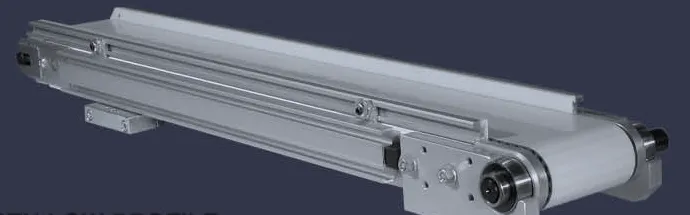
Precision indexing
Stops parts where the work happens.
A timing-belt conveyor that advances, stops at working positions, reverses and runs in step with other conveyors.
- Belt
- Timing belt
- Motion
- Index, dwell, reverse
- Profiles
- 17 or 25 tooth low profile
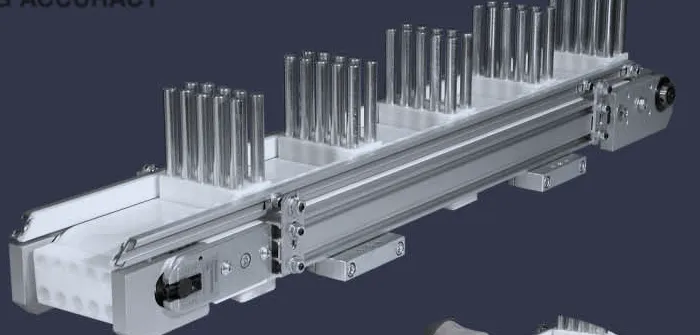
Part holding
Holders that come off by hand.
Parts ride in guided holders located to tight tolerances. When the part or operation changes, the holders change without tools.
- Typical positioning
- ±0.01 in
- Holder change
- Without tools
- Patent
- U.S. 6,321,904
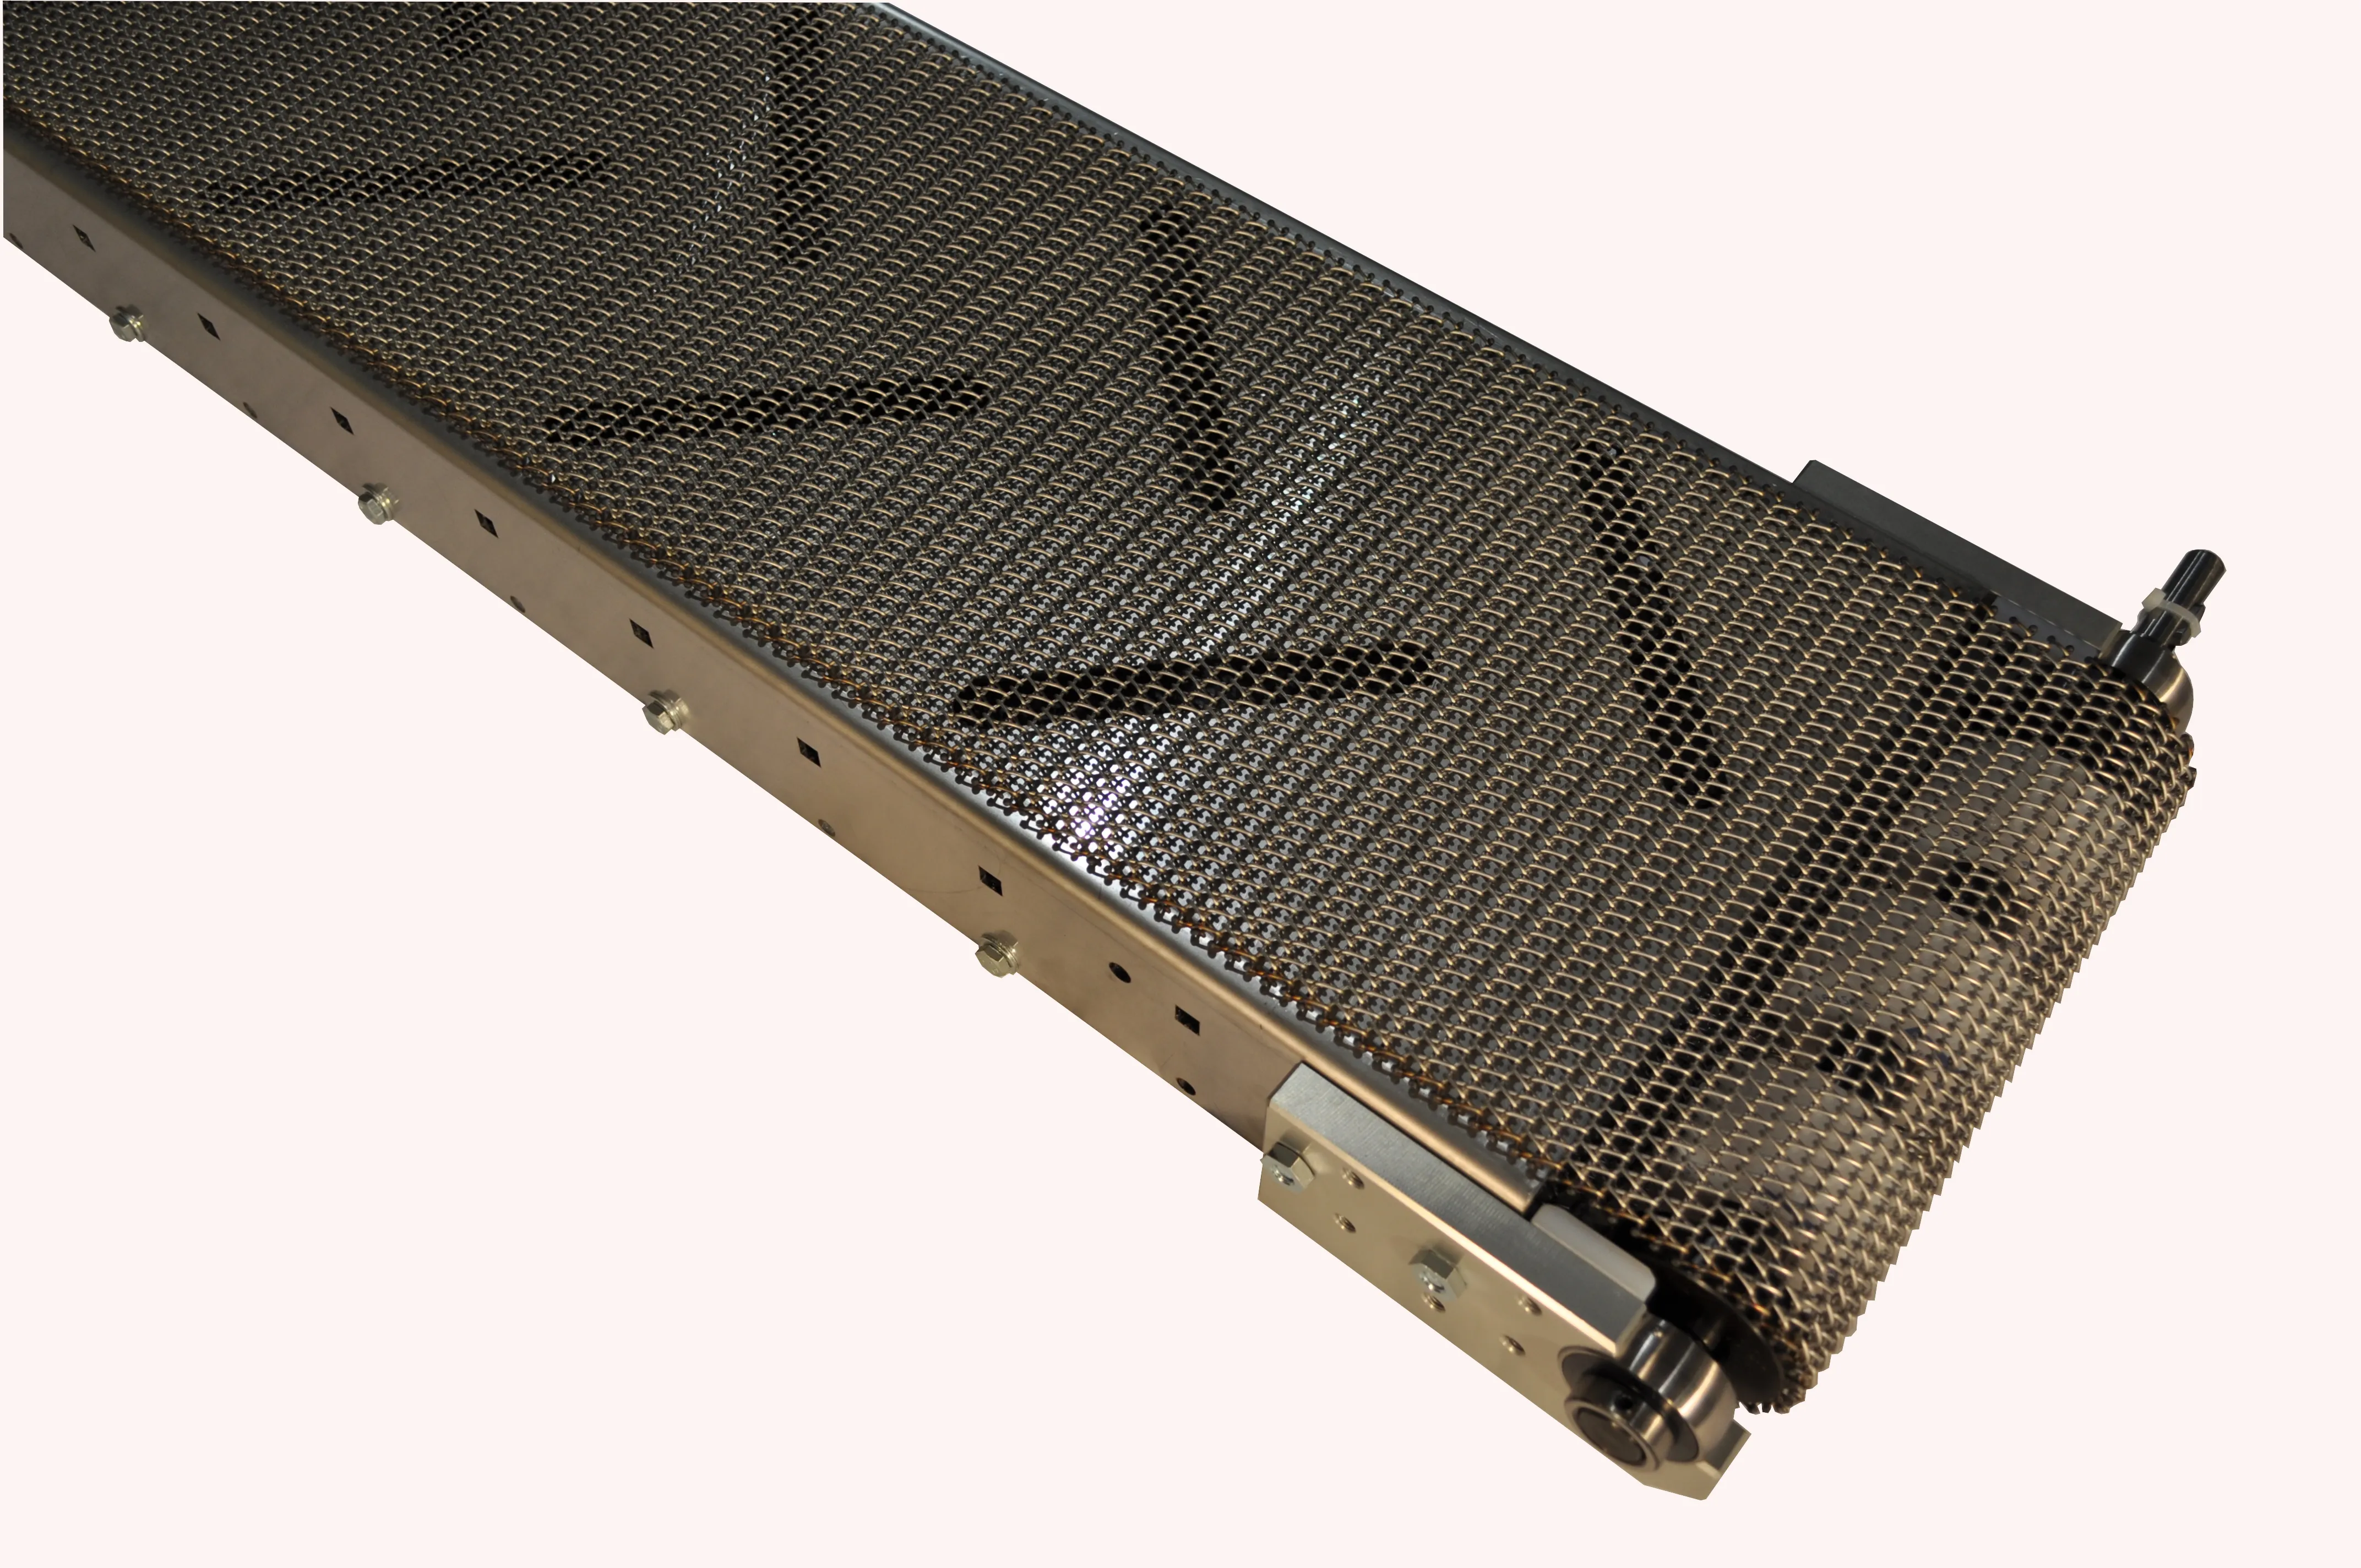
Hot, wet and oily parts
Air and fluid pass straight through.
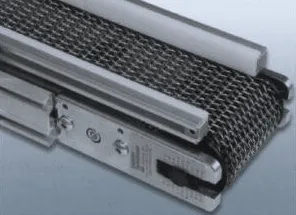
An open stainless steel belt for hot parts, cooling and draining wet or oily components, with guides rated by temperature.
- Belt
- Stainless steel mesh
- Stainless guides
- Parts to 1000°F
- Use
- Cooling and drainage
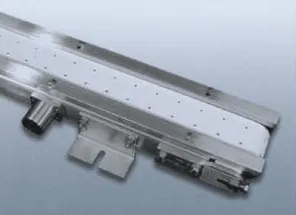
Light parts
Holds parts without touching the top.
Suction through a patterned belt keeps light or unsteady parts in place and in orientation as they travel.
- Hold
- Suction through the belt
- Pattern
- Matched module and belt
- Load
- Up to 50 lb
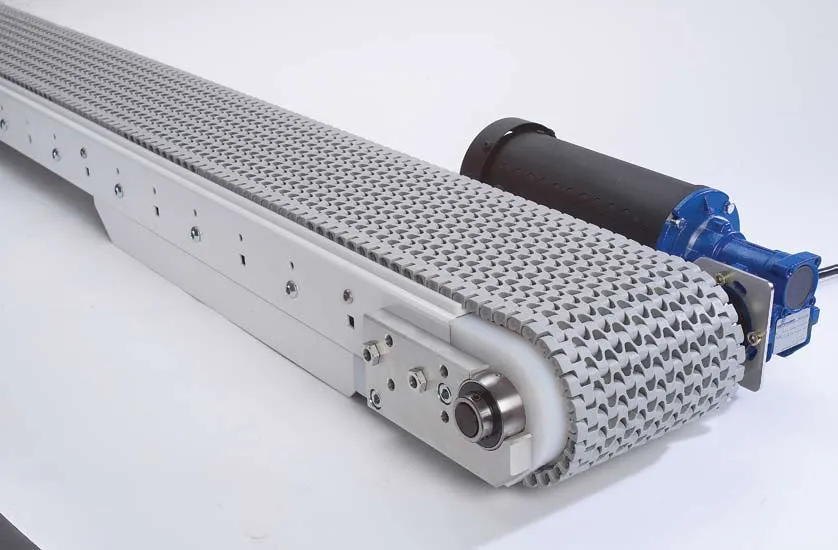
Washdown
Surfaces for every product.
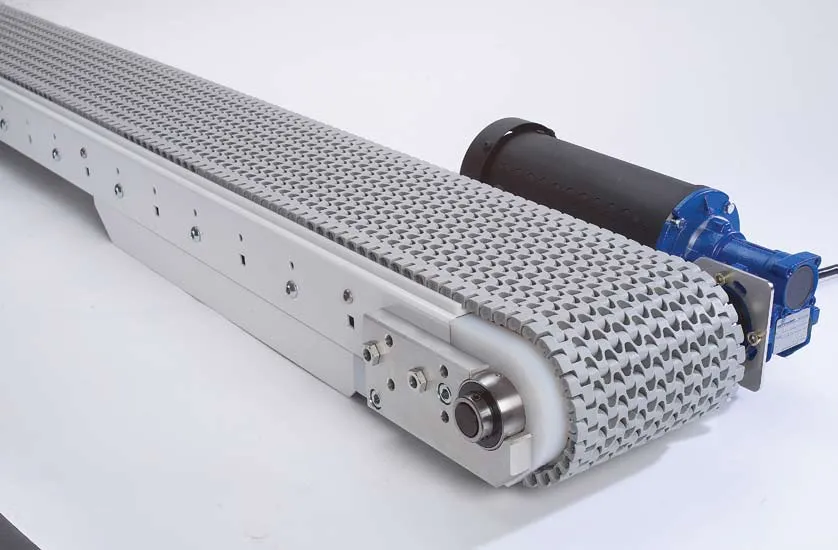
Interlocking plastic modules in eight surfaces and four materials, with belts that change in minutes without tools.
- Surfaces
- 8 styles
- Pitch
- 0.5 or 1.0 in
- Load
- Up to 300 lb
On your line
From the machine that makes it to the one that uses it.
Six jobs a conveyor does between operations. We design for the one you need, or all six.
Receive
Catch it as it drops
Parts, runners and scrap below the mold or press.
Hold
Keep it where you put it
Holders, vacuum or cleats keep each part located.
Index
Stop at every station
Advance, stop in position, work, move on.
Inspect
Give the camera a clean view
Light from inside the belt outlines every part.
Cool & drain
Let air and fluid through
Open mesh for hot, wet or oily parts.
Transfer
Hand it to the next machine
Drive wherever the machine leaves room.
Family-ownedTwo generations
About us
Two generations. One standard.
Charles Mitchell founded Conveyor Technologies to end conveyors that needed constant attention. His son Anthony leads the company today, and works directly with customers on system design and troubleshooting.
Every conveyor is judged by one question: how easily can it be kept running?
01Founded in Milford
Charles Mitchell sets out to end high-maintenance conveyors.
02One modular system
Components that interchange across conveyor types.
03A complete range
Indexing, inspection and specialist conveyors.
TodayNext generation
Anthony Mitchell leads the company.